Specifying oem carbon air pro pickleball paddle factory for Wholesale and OEM Orders
The limiting factor is rarely the headline specification. While buyers focus on weight, the structural integrity of the carbon fiber weave determines the long-term response rate under repetitive impact stress. A vacuum-molded process ensures the resin distribution remains uniform, preventing dead spots across thousands of units. Consistency in the honeycomb core density reduces the rate of defective units in high-volume shipments.
Procurement officers must evaluate the thermal stability of the bonding agents between the carbon face and the polymer core to prevent delamination in high-ambient-temperature outdoor play conditions.
Measured Performance in Real Use
Weight and stiffness trade off against each other. A 16mm polymer honeycomb core increases energy absorption but raises the swing weight. Conversely, a 13mm core provides more power at the cost of vibration-induced fatigue over time. The balance point dictates whether the paddle serves a defensive or offensive retail market segment.
Core Thickness
13mm variants offer maximum ball pop; 16mm variants prioritize control and dampening for tournament players.
Face Material
T700 carbon fiber provides high tensile strength compared to standard fiberglass-based composites.
Surface Friction
Raw carbon fiber textures increase spin rates through friction friction coefficients that wear over time.
Matching the Product to the Buyer's Need
Selection strategy depends on the target demographic's skill level. Recreational-grade paddles benefit from larger sweet spots and lighter frames to reduce wrist strain. Professional-grade orders require specific swing weight tolerances and aerodynamic edge guards to withstand high-velocity play.
- Request perimeter weighting via foam injection for increased stability in elite-tier models.
- Utilize moisture-wicking grips to maintain surface integrity during extended summer sessions.
- Custom UV-curable printing requires specific inks to prevent fading under prolonged sun exposure.
Buying Mistakes That Lead to Returns
Repeat loading drives the failure. Low-grade adhesive layers often delaminate after 50 hours of high-velocity play when temperature fluctuations occur. High-thermal bonding secures the carbon face to the honeycomb core to prevent edge separation. Failing to inspect the edge guard attachment points results in high return rates from distributors.
Price-per-unit analysis often hides inconsistent core density. Inconsistent cell structures leads to unpredictable bounce heights across a batch, which devalues brand reputation for OEM owners.
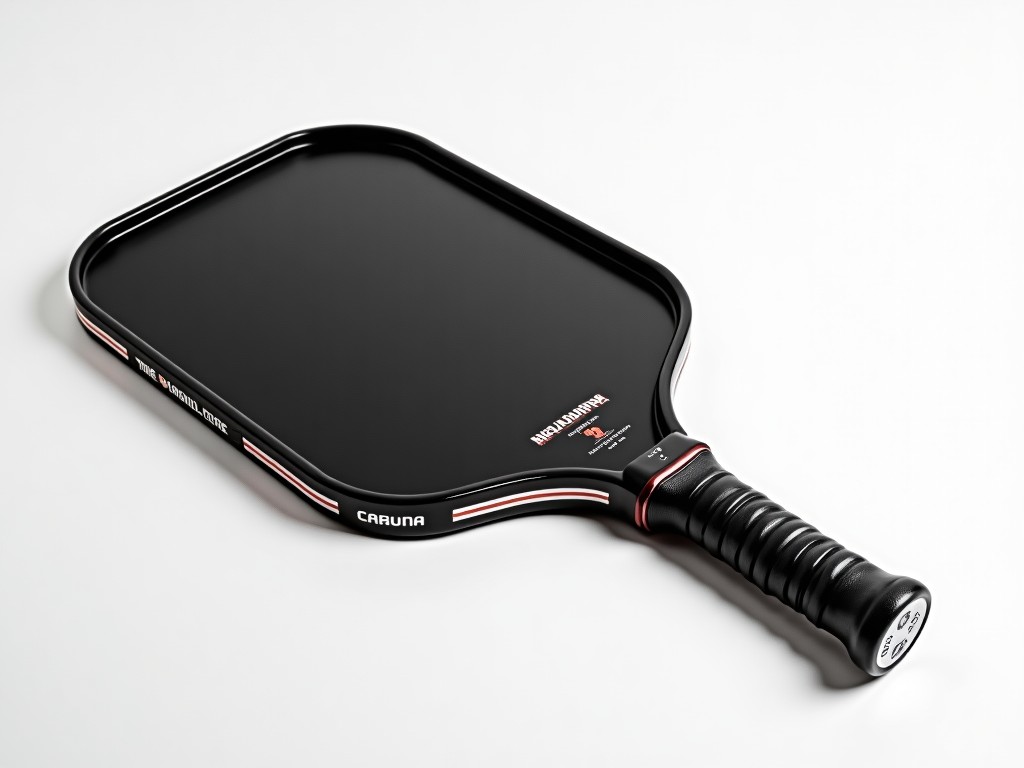
Segment-Specific Requirements
| Finish Type | Application Segment | Performance Metric |
|---|---|---|
| Textured Raw Carbon | High-Spin Competitive | Maximum Friction Coefficient |
| Matte Painted | Retail/Club | Visual Durability |
| Glossy Coat | Entry-Level | UV Resistance |
Volume Planning and Lead Time
Production cycles scale with the complexity of the carbon layup. Standard OEM molds typically require a 30-45 day lead time for orders exceeding 1,000 units. Custom tooling for unique face shapes adds six weeks to the initial development phase. Freight-logistics planning should account for seasonal demand spikes in the sports market.
To discuss technical specifications or batch consistency protocols, initiate a project discussion regarding your carbon fiber paddle requirements.


