Custom left handed tennis racket Factory: What Buyers Should Check Before Ordering
Manufacturing Trade-off: Producing left-handed frames requires precise recalibration of the layup orientation to maintain the intended balance point. While mirrored production ensures structural symmetry, it often increases tooling setup time by 15-20% compared to right-handed-only high-volume production runs.
Design Constraints Behind the Specification
Repeat loading drives the failure in frames where the carbon fiber orientation is not optimized for specific impact vectors. For left-handed players, the torque distribution during the reverse backhand creates unique stress on the throat joint. If the 24T layup does not reinforce these lateral cross-sections, the frame risks delamination within the first 500 high-impact cycles.
High-modulus carbon fibers increase frame stiffness but elevate vibration transfer to the player. Brand managers must balance this by integrating viscoelastic dampening layers in the mid-section to prevent fatigue without adding significant swing weight. This balance determines the final reorder rate for professional-grade rackets.
Size, Weight and Specification Range
Standard production ranges vary based on the market segment, from recreational to competitive tournament play. Factories typically offer head sizes from 95 to 105 square inches to accommodate different sweet-spot tolerances and stability requirements. Beam widths fluctuate from 20mm to 26mm, affecting the aerodynamic drag and the potential for ball launch power.
| Parameter | Standard Range | Tolerance Tolerance |
|---|---|---|
| Total Weight | 280g - 340g | +/- 2g |
| Head Size | 95 - 105 sq in | +/- 1 sq in |
| Balance Point | 310mm - 350mm below grip | +/- 5mm |
| Beam Width | 20mm - 26mm | +/- 0.5mm |
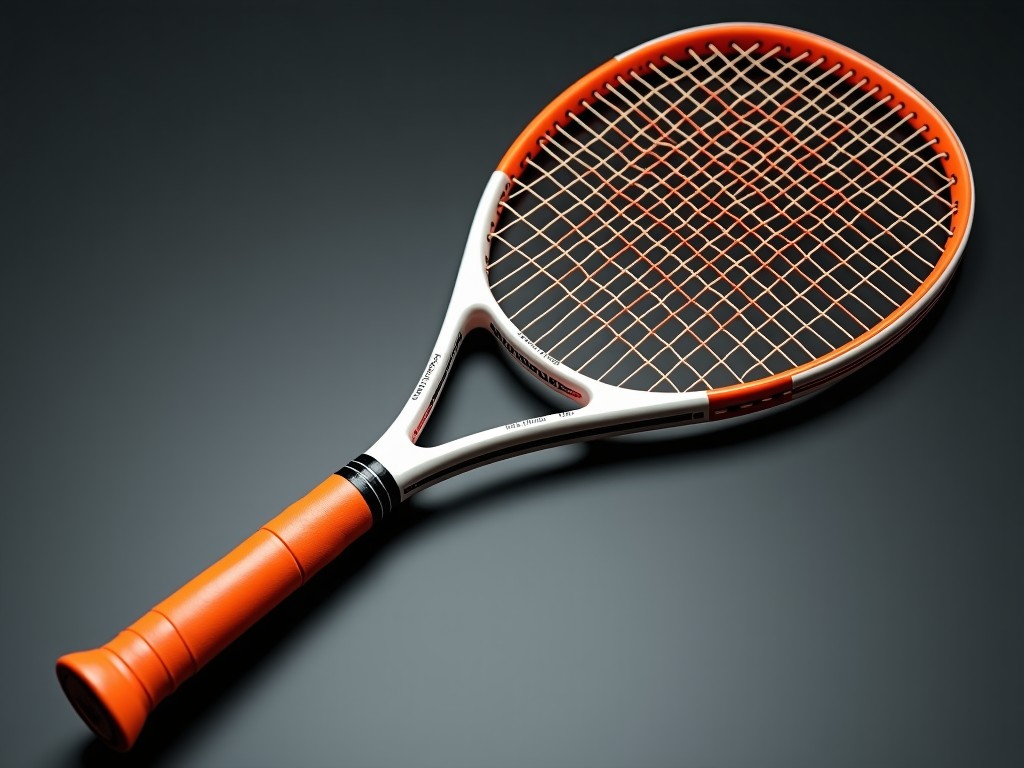
Comparing Two Standard Configurations
Buyers often choose between control-oriented frames and power-oriented frames. A control frame utilizes a thinner beam and a higher balance point to provide stability on heavy shots. Conversely, a power frame employs a wider beam and head-weight to increase ball exit velocity.
Control Configuration
Focuses on precision and feel. The lower stiffness rating (RA value) allows for more dwell time, providing better accuracy for players with fast swing speeds.
Power Configuration
Utilizes higher stiffness and aerodynamic profiles to maximize energy return. Ideal for players seeking more depth on shorter baseline strokes.
Customisation Options and Their Limits
Weight and stiffness trade off against each other during the customization phase. Adding lead weight to the head increases swing weight but alters the balance point, potentially leading to hoop instability. Customizing the grip size requires modifications to the internal handle mold to maintain structural integrity under high tension.
Surface finishes include matte powder coatings or high-gloss UV-resistant paints. However, the durability of the paint is dependent on the adhesion strength of the primer layer applied to the carbon fiber. Poor preparation results in chipping when the racket contacts the ground or court surface.
Quality Control and Batch Consistency
Batch consistency is maintained through automated weight and balance testing post-painting. Every left-handed frame undergoes a tension test to ensure the throat can withstand 55-60kg of pull without permanent deformation. This prevents the common "soft frame" complaint found in lower-tier manufacturing runs.
Visual inspection uses ultrasonic scanning to detect internal voids in the resin-fiber matrix. If the internal density variance exceeds 3%, the unit is rejected. This rigorous QC process reduces the rate of warranty claims for the brand owner over the long term.
Keeping Repeat Orders Supplied
Reliable supply depends on the traceability of raw carbon prepreg and resin. By tracking batch numbers, the factory ensures that the second order matches the material modulus of the first approved sample exactly. This consistency is vital for brands maintaining a uniform product line across multiple regions.
Packing, Marking and Freight Configuration
Export-grade packaging utilizes corrugated cardboard sleeves with internal dividers to prevent friction damage during sea transit. Each racket is marked with technical specifications, including weight and balance, to facilitate rapid inventory management. Retail-labeling is applied at the final stage to allow for regional market flexibility by the distributor.
Questions Buyers Ask Before Ordering
- What is the MOQ for custom left-handed molds? Typically 500 units per specification are required to offset the cost of mirrored CNC-machined molds.
- How do you ensure grip size consistency? We use injection-molded handles with precision inserts to ensure the internal dimensions remain constant across entire production batches.
- What is the lead time for custom paint schemes? Standard production cycles run from 60-90 days depending on the complexity of the coating application and curing times.
Ready to finalize your technical specifications and production schedule?
Request artwork and branding review

