low price pro staff power tennis rackets for sale: Specification, Ordering and Quality Notes
Where chlorine, sweat or UV exposure is routine, the structural integrity of a tennis frame determines the retail lifecycle. Pro-level power-oriented rackets designed for bulk distribution require a balance between high-modulus graphite construction and cost-effective manufacturing de-optimization. For distributors and OEM buyers, the focus shifts from aesthetic de-tailing to the frame's ability to withstand high-tension stringing cycles without delaminating or losing its balance point.
Design Constraints Behind the Specification
Stiffness-Mass Trade-off
A wider beam width (26mm+) increases hoop stability and power return but elevates the unstrung weight. To maintain a "pro staff" feel at a 300g-315g range, the layup utilizes variable thickness in the throat to prevent excessive flexibility without adding unnecessary head mass.
Selecting a specific RA rating (stiffness) dictates the comfort profile for the end-user. A frame exceeding 70 RA provides energy return but increases the risk of frame cracking if the resin-to ratio is too brittle. Procurement officers must weigh the cost of higher-grade carbon fibers against the required durability of the frame to survive the high-impact loads common in club-level play.
Construction Method and Its Effect on Consistency
Pre-preg carbon fiber layup offers more consistent resin-to-fiber ratios, reducing the weight fluctuations found in wet-layup methods. This process ensures that every racquet in a batch stays within a +/- 3g weight tolerance. In lower-tier manufacturing, inconsistencies in internal hollow sections often lead to air pockets, which become failure points under the tension of 55kg strings.
Internal vibration dampening systems integrated during the molding process prevent the frame from becoming brittle over time. When these materials are bonded directly to the graphite layers, they maintain the structural modulus of the frame, ensuring the "power" of the racket remains consistent even after 100 hours of active use.
Measured Performance in Real Use
| Inspection Method | Metric | Tolerance Range |
|---|---|---|
| Static Tension Test | Frame Rebound | +/- 5% deviation |
| Weight Analysis | Unstrung Mass | +/- 3 grams |
| UV Exposure Cycle | Color Fastness | Delta E < 2.0 |
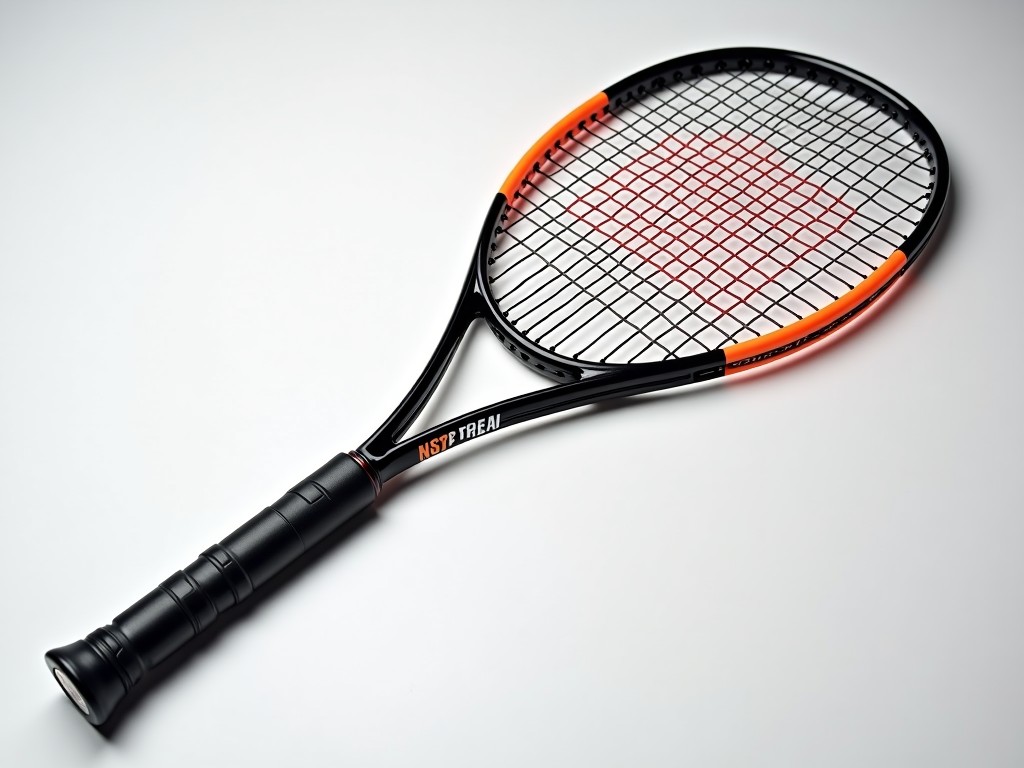
Buying Mistakes That Lead to Returns
Ignoring the quality of the grommet system is a primary cause of field failures. Cheap plastic grommets tear under tension, allowing the strings to cut into the graphite frame, which renders the racket unsafe immediately.
- Using low-grade epoxy finishes that peel after exposure to sweat-based acids.
- Accepting variable balance points which lead to inconsistent "feel" for players.
- Neglecting the throat reinforcement, leading to stress fractures during heavy serves.
- Prioritizing aesthetic paint over the structural integrity of the base coat.
Working as a Production Partner, Not a Catalogue Supplier
Effective OEM partnerships require a rigorous technical approval phase before the first mold is cut. We provide detailed CAD drawings that specify wall thickness at every point of the frame. This prevents the "guess-work" manufacturing often seen in low-price rackets that fail prematurely under mechanical stress.
By reviewing the specific requirements of your target demographic, we can adjust the fiber orientation to prioritize either stiffness or flexibility. This proactive approach ensures that the "pro staff" label does not come at the expense of structural reliability, reducing return rates.
How Consistency Is Held Across Batches
- Every batch undergoes a weight-distribution check to ensure the center of gravity remains uniform.
- Automated curing cycles monitor temperature and pressure to maintain resin density across all units.
- Randomized impact testing verifies that the frame modulus matches the approved master sample specification.
Capacity, Tooling and Scheduling
Production lead times are dictated by the complexity of the steel molds required for custom geometries. For standard frames, tooling typically requires 4 to 6 weeks. Once the tooling is validated, our capacity allows for scalable monthly runs of up to 5,000 units per model without compromising the precision of the layup process.
Review our tooling specifications and production timelines.


