OEM atomica advanced tennis racket Exporter: What Buyers Should Check Before Ordering
Consistency is set at the forming stage where the orientation of carbon fiber sheets determines the frame's torsional stiffness. If the layup sequence is inconsistent, the racket exhibits unpredictable vibration de-coupling during high-impact serves, leading to high return rates from retail-level de-registration.
First-article tooling determines the precision of the internal hollow geometry where the weight distribution occurs. Poorly machined steel molds lead to variations in beam width, which directly impacts the string tension stability and overall aerodynamic consistency across a production run of 5,000+ units.
Materials and Construction Trade-offs
High-modulus graphite increases the stiffness-to-weight ratio but increases the risk of brittle fracture under extreme shock-loading. Standard modulus carbon offers more flexibility for better energy return but requires additional mass to achieve similar power ratings, which increases the swing weight for the end user.
Structural Integrity Note
Using pre-preg resin systems instead of hand-saturated fabrics reduces resin pockets by 12%, which prevents delamination at the throat despite the slight increase in raw material cost per frame.
Comparing Two Standard Configurations
Atomica-Power Series
- Wide beam width of 28mm for maximum Sweet Spot.
- Head-heavy balance point at 320mm.
- Stiff frame rating (300 RA) for ball velocity.
Atomica-Control Series
- Aerodynamic beam width of 22mm for precision swing.
- Even-balance point at 315mm.
- Flexible frame rating (610 RA) for vibration dampening.
Customisation Options and Their Limits
Customizing finishes involves water-transfer applications that maintain the structural integrity of the carbon weave. However, adding thick paint layers adds 3-5 grams to the frame, which can shift the calibrated balance point.
- UV-resistant clear coats prevent pigment fading over 24 months of outdoor exposure.
- Custom grommet patterns allow for specific string tension adjustments but increase assembly time.
- Weight-drilling in the head allows for post-production balancing but creates stress points.
Quality Control and Batch Consistency
Batch consistency is measured by a weight tolerance of ±2 grams and balance point variance of +/- 3mm. Deviations exceeding these limits result in frame rejection to ensure a uniform feel across the entire retail order.
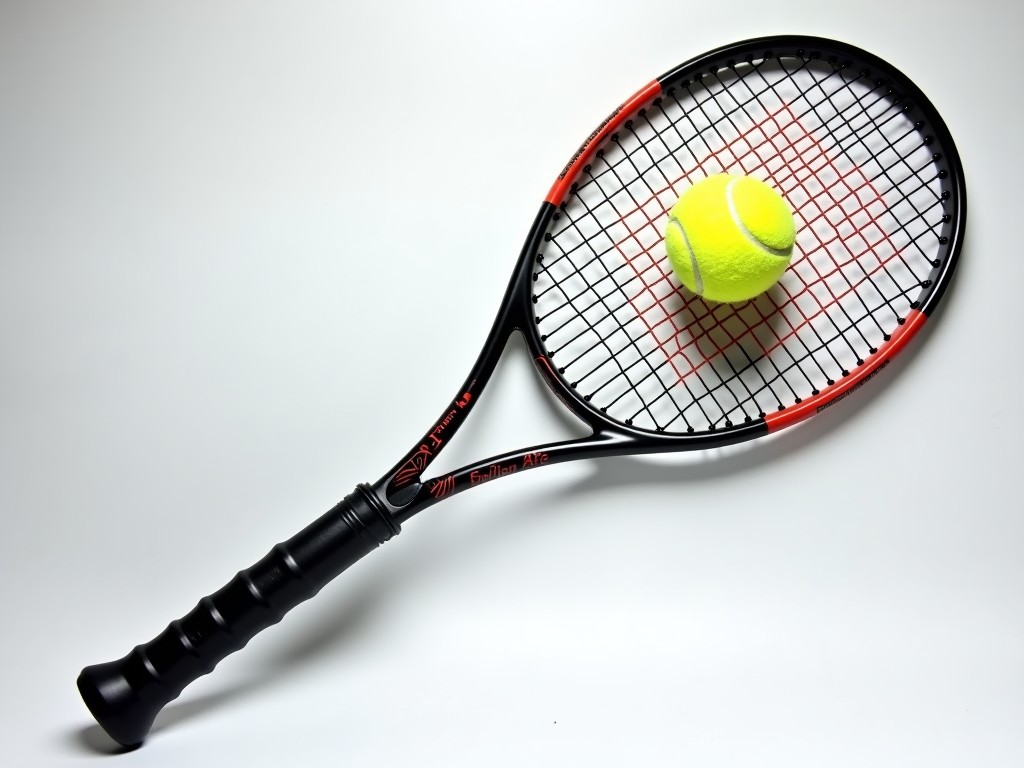
What Gets Checked Before Shipment
| Inspection Metric | Acceptance Criteria | Testing Method |
|---|---|---|
| Frame Integrity | No visible cracks or fractures | Static load test |
| Paint Adhesion | No delamination at 5kg | Cross-hatch tape test |
| Tension Capacity | Up to 60kg stable | Digital tension gauge |
Capacity, Tooling and Scheduling
Steel mold production for new geometries requires 45-60 days of lead time. Once tooling is active, the monthly output capacity reaches 2,500 units per line based on the number of autoclave cycles available.
Ordering, Tooling and Lead-Time Questions
What is the minimum order quantity for custom branded rackets?
Custom branding requires 500 units per specification to offset the setup cost of specialized silk-screen plates.
How are the rackets packed to prevent transit damage?
Each racket utilizes double-walled corrugated cardboard with individual foam sleeves to prevent frame-to-frame impact abrasion during sea freight.


